0.2 copper straight onto a Jiashikai negative — I’m telling you, don’t try it! It just won’t hold…


Creator’s own settings as stated in the video (timestamps link to the moment). Not official values — test on scrap first.
Bill of materials
Welder, accessories, consumables and parts used in this build; quantities and specs are editable Download BOMDescription
Lefeng puts 0.2 copper + 0.15 nickel-plated straight onto a Jiashikai negative with the P60F: gear 400 sticks the pins and the nickel strip is pierced without the copper bonding; thinner nickel at gear 450 still won’t take, “these holes crack me up”; preheat adjusted, gear 600; gear 700 “burnt black, way too strong” but finally can’t be pulled off, cuts his hand, the 0.2 copper tears into a hole before it counts as welded — “I’m telling you, don’t try it, the current is too high”; comments: weld the copper first then the nickel / use thick 3mm round-tip pins / your skills are questionable
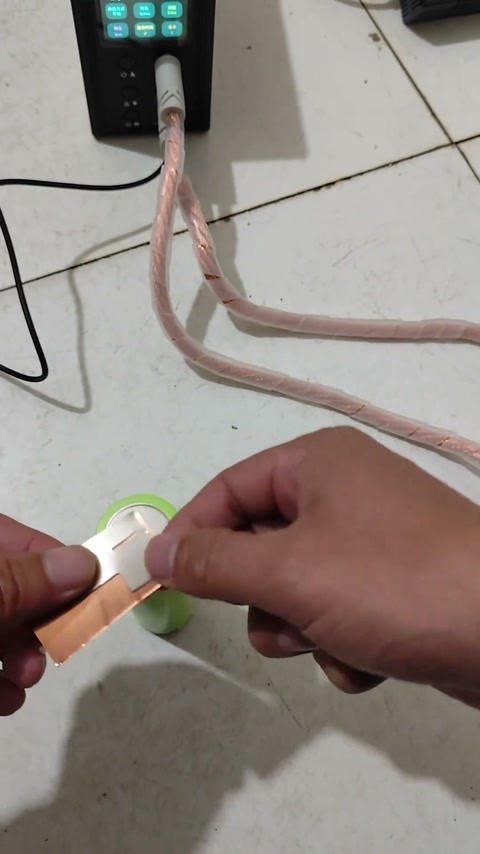
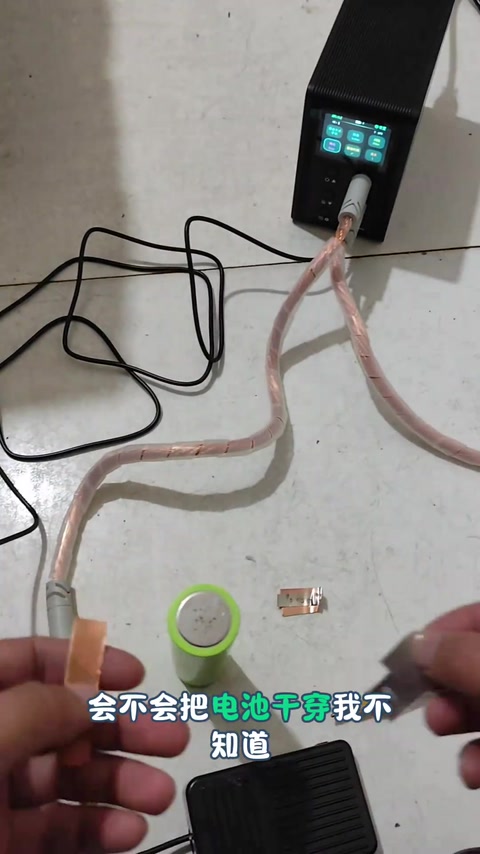
I’m telling you not to try this: this time 0.2 copper sheet plus 0.15 nickel-plated steel strip goes straight on, no nickel base layer; a test weld first, the cell wasn’t sanded, it just has a few old holes from before; the welder is an AWithZ P60F, gear 400, preheat 0.1, interval 1ms; before he even welds, someone says it won’t hold; the current is fierce, you can’t go in square-on or it burns right through the sheet, keep the pens as flat as possible; the pins stuck; it didn’t bond but the nickel strip was pierced clean through, the technique must be wrong, 0.2 copper and nickel both burned with holes and still no bond, or maybe I don’t know how to run the machine; an internal-resistance meter (HRM-10) reads the cell at 3.32V; swap to thinner nickel strip and try, still 0.2 copper strip, gear 450, looks like it might take this time? no, it won’t, forget it, these punched holes crack me up; back to the nickel-plated steel strip, I refuse to believe it; adjusted the preheat, gear 600, whether it’ll punch through the cell I don’t know, getting a bit annoyed after it wouldn’t hold; gear 700: this looks burnt black, too big, too strong; truly can’t be pulled off, cut my hand; now it really won’t come off, the copper stuck to the top, the 0.2 copper strip torn right into a hole; if that’s not enough I’ll add another 100 gears, that’ll definitely do it; so that’s why I tell you not to try 0.2 copper lightly, it just blew two holes, and at gear 700 the current is still too high. 308 comments: if this welder can weld 0.2 copper, every spot-welder seller online can shut down (2); my ¥100-odd unit does 0.1 stacked on 0.1 copper no sweat (2); your skills are questionable; bought a UF20B after your video and it can’t weld 0.1 + 0.1; 0.2 copper + 0.15 nickel-plated won’t take, add 0.1 nickel-plated and you still need flux paste; pins too thin, use 3mm round tips; 700 works, thick pins are best; weld the copper first then the nickel (are you serious?); test the Xiaoqiang; a four-capacitor rig welds it instantly.
Outcome
| Goal | Explore P60F gears for 0.2 copper + 0.15 nickel-plated welded straight onto a Jiashikai negative |
| Build | P60F + 0.2 copper + 0.15 / thinner nickel-plated + Jiashikai 32140 |
| Result | Gears 400/450/600 don’t hold; gear 700 is too strong and burns black but can’t be pulled off; verdict is not to put 0.2 copper straight on · verified on camera: 99–125s, 198–220s failures; 320–371s tear at gear 700 |
Steps6 steps · click a frame to jump
 1. Setup: 0.2 copper + 0.15 nickel-plated straight on; P60F gear 400, preheat 0.1, interval 1ms
Warns not to try this lightly; 0.2 copper sheet plus 0.15 nickel-plated steel strip straight on, no base layer; the cell isn’t sanded and has old holes; AWithZ P60F, gear 400, preheat 0.1, interval 1 millisecond.
00:00 – 00:43 2. Gear 400: fierce current, keep it flat; pins stick; nickel pierced, copper not bonded — technique or machine
Someone says it won’t hold; the current is fierce, don’t go in square-on or it burns through, keep it as flat as possible; the pins stuck; no bond but the nickel strip was pierced through; must be the technique; 0.2 copper and nickel burned with holes and still no bond; or maybe I can’t run the machine, try again.
00:43 – 02:13 3. Cell reads 3.32V; thinner nickel strip at gear 450: still won’t take, “these holes crack me up”
Which step is going wrong; HRM-10 reads the cell at 3.32V; swap to thinner nickel strip, still 0.2 copper strip, gear 450; looks like it might take this time? no, forget it, these punched holes crack me up.
02:20 – 03:20 4. Back to 0.15 nickel-plated, refuses to believe it; preheat adjusted, gear 600, worried about punching through, annoyed
Back to this nickel-plated steel strip, I refuse to believe it; adjusted the preheat, gear 600, no idea whether it’ll punch through the cell; a bit annoyed after it wouldn’t hold.
03:40 – 04:26 5. Gear 700: burnt black, too strong; truly can’t be pulled off; cuts his hand
Gear 700; this is burnt black, too big, too strong; truly can’t be pulled off; cut my hand; now it really won’t come off.
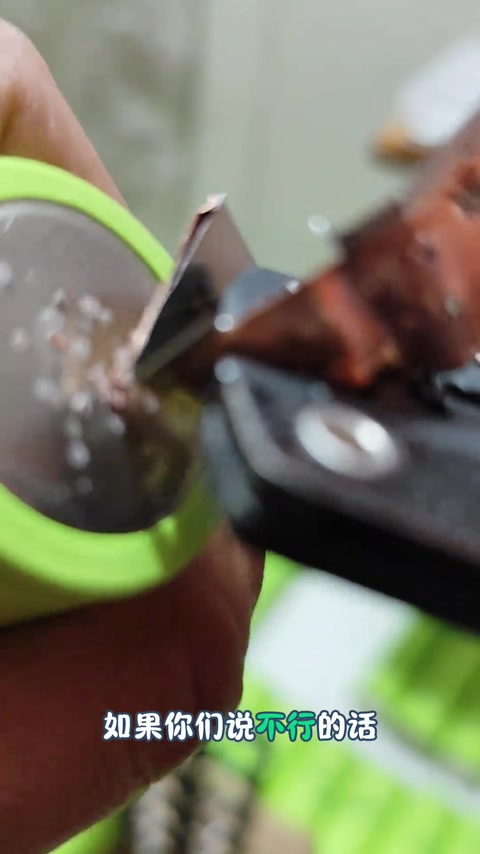
04:50 – 05:49 6. 0.2 copper torn into a hole counts as welded; another 100 gears would do it too; gear 700 current still too high — don’t try it lightly
Looking at the result, the copper stuck to the top, the 0.2 copper torn right into a hole; if not enough, add another 100 gears, that’ll definitely do it; so that’s why I tell you not to try 0.2 copper lightly, it just blew two holes; gear 700 is still too big, current too high.
05:49 – 06:33
Bill of materials
| AWithZ P60F ×1 | Gears 400–700 · Direct stacked-copper test |
| Copper sheet 0.2 | Welded straight on |
| Nickel-plated steel strip 0.15 / thinner | Top layer |
| Jiashikai 32140 ×1 | Steel-can negative · Test cell |
| HRM-10 internal-resistance meter ×1 | Test the cell |
Measured on camera
| Cell voltage | 3.32 V 02:20 |
Creator’s tips
- For high-current stacked welds keep the pens as flat as possible; square-on burns through easily 00:57
- 0.2 copper straight onto a Jiashikai negative needs gear 700 or so and burns black — not recommended; comments suggest 3mm round-tip thick pins 05:20
Pitfalls
- Gears 400/450/600 all failed to hold; the nickel strip was pierced / punched with holes 01:39
- Gear 700 burns black; cut his hand 05:20
- Comments: bought a UF20B after the video and it can’t weld 0.1 + 0.1; 0.2 + 0.15 only works with flux paste
Li-ion safety
- High gears may punch through the cell; cut hands while handling 04:07